
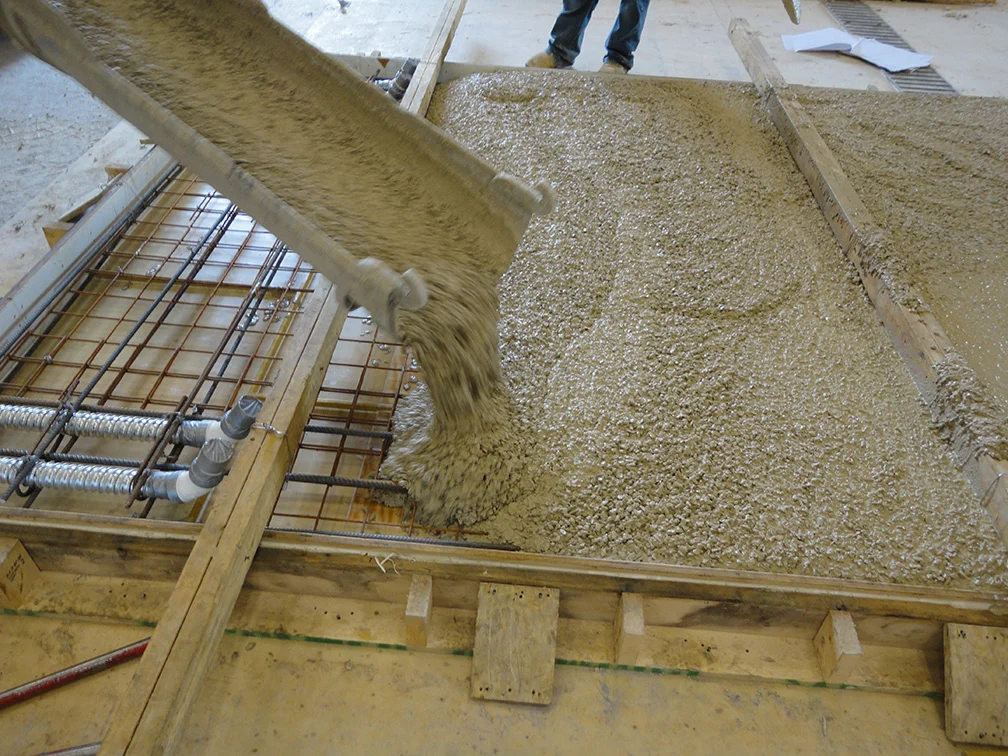
An admixture is a performance contract, not a magic ingredient. ASTM C494/C494M sorts chemical admixtures into eight classes, and each class comes with measurable limits on water reduction, setting time and strength that the product has to hit against a control mix. Knowing those limits tells you what you are buying — and, just as usefully, what you are not.
This matters more here than in a milder climate. In Calgary a slab can be placed at 4 °C in the morning and finished under a chinook at 15 °C by mid-afternoon. The admixture package that holds that pour together is doing different work at hour one than at hour four, and getting it wrong shows up as a finishing window that closes early, a set that never arrives before dark, or a surface that dusts in spring.
The eight ASTM C494 types, in plain terms
ASTM C494 classifies admixtures by what they do to water demand and setting time, not by chemistry. Two products with entirely different chemistry land in the same type if they produce the same measured effect.
| Type | Name | What it does |
|---|---|---|
| A | Water reducing | Same slump at lower water content |
| B | Retarding | Delays set, no water reduction claimed |
| C | Accelerating | Speeds set and early strength gain |
| D | Water reducing and retarding | Type A effect plus delayed set |
| E | Water reducing and accelerating | Type A effect plus faster set |
| F | Water reducing, high range | Large water reduction (superplasticizer) |
| G | Water reducing, high range, and retarding | Type F effect plus delayed set |
| S | Specific performance | Everything else with a defined performance claim — slump retention, shrinkage reduction, viscosity modification |
Type S is the catch-all that lets modern products qualify without distorting the older categories. A slump-retaining admixture that holds workability for 90 minutes without pushing set time back is a Type S product; it does not fit Type B or Type G, because it is not supposed to retard.
What the standard actually requires
The numbers behind the type letters are where the specification stops being marketing. ASTM C494 measures a trial batch against a control batch of the same materials and applies these limits:
| Requirement | Type A / D / E | Type F / G | Type B |
|---|---|---|---|
| Maximum water content, % of control | 95% | 88% | — |
| Implied minimum water reduction | 5% | 12% | none claimed |
| 3-day compressive strength, min % of control | 125% (A, E); 110% (D) | 125% | 90% |
| 28-day compressive strength, min % of control | 110% (A, D); 100–110% (E) | 100–110% (F); 110% (G) | 90% |
Read the water-reduction line carefully. A Type A water reducer only has to get you 5% below the control water content. In practice a good normal-range product gives 5–8%, a mid-range product gives 8–12% while still qualifying only as Type A, and a high-range product has to clear 12% to be a Type F at all — with real-world high-range products commonly delivering 12–40% water reduction depending on dosage and mix.
That difference is not academic. On a 32 MPa mix, cutting water 12% instead of 5% is the difference between hitting your water-to-cementing-materials ratio comfortably and chasing it with extra cement.
Setting time is bounded too, relative to the control:
| Type | Initial set, relative to control |
|---|---|
| A, D, F | From 1:00 earlier to 1:30 later |
| B | 1:00 to 3:30 later |
| C, E | 1:00 to 3:30 earlier |
| G | 1:00 to 3:00 later |
So a Type C accelerator is guaranteed to pull initial set forward by at least an hour, and is not permitted to pull it forward by more than three and a half. If you need more than that, you are not looking for an accelerator — you are looking for a different cement type or a heated mix.
Water reducers: normal, mid-range and high-range
The practical dividing line is what you want the water reduction to buy you. All three classes remove water; they differ in how much, and in what happens to slump over time.
- Normal-range (Type A). 5–8% water reduction. Steady, forgiving, cheap. The default on residential flatwork and footings. Some Type A products increase the rate of slump loss, which matters on a long haul or a hot day.
- Mid-range (still qualifies as Type A). 8–12% reduction with noticeably better finishability. Popular for exposed flatwork and pumped placements where you want workability without the slump-loss behaviour of a high-range product.
- High-range (Type F and G). 12% and up, often far more. This is what makes low water-to-cementing-materials ratio mixes placeable at a workable slump — self-consolidating concrete, dense C-1 exposure mixes, tight rebar in structural elements.
The trade-off with high-range products is time. A Type F superplasticizer produces a dramatic slump increase that decays faster than a normal water reducer’s, so it is often added at site rather than at the plant. Type G exists precisely to buy back that time by retarding the set alongside the water reduction.
If the mix is being selected for durability rather than placement, the water-to-cementing-materials ratio and the exposure class drive the decision first — see our breakdown of the CSA A23.1:24 exposure classes and which one your project actually needs. The admixture then makes that ratio placeable.
Accelerators, and the chloride question
Accelerators fall into two camps in Alberta, and the split is about corrosion, not speed.
Calcium chloride is the classic accelerator: cheap, effective, and restricted. Concrete Saskatchewan’s guidance caps it at 2% by weight of cement in non-reinforced concrete, and is explicit that prestressed concrete and concrete containing embedded aluminum or galvanized metal should not contain any chloride-based materials at all. Manitoba Infrastructure’s cast-in-place concrete specification goes further and prohibits calcium chloride and accelerators outright unless the engineer approves them, while capping water-soluble chloride ion content at 0.15% by mass of cementitious material across all concrete types.
That is why non-chloride accelerators dominate structural work here. They cost more per cubic metre for less acceleration, but they leave the chloride budget alone — which matters on a project already carrying chloride exposure from de-icing salts.
Where accelerators earn their keep in Calgary:
- Late-season flatwork where the finishing crew needs to be off the slab before temperatures drop after sunset.
- Cold-weather pours where you are paying for heat and hoarding, and every hour of protection removed is real money.
- Early stripping of forms on a tight cycle, where 3-day strength governs the schedule.
Where they do not help: an accelerator does not replace protection. Concrete still has to be kept warm enough to hydrate. CSA A23.1’s basic curing regime asks for three days at 10 °C or until the concrete reaches 40% of specified strength; additional curing asks for seven days at 10 °C and 70% of strength. An accelerator shortens the clock, it does not stop it. Our cold-weather concrete rules for Calgary crews covers the protection side in detail.
Retarders, and why Alberta needs them in summer
A retarder buys placing and finishing time when ambient conditions are stealing it. ASTM C494 Types B and D delay initial set by at least an hour, and most retarders also function as water reducers — which is why Type D, the combined class, is more commonly supplied than a straight Type B.
Calgary’s summer conditions are deceptive. Air temperature rarely reaches the extremes seen further south, but humidity is low, wind is frequent, and the elevation raises solar intensity — a combination that drives high evaporation from a fresh surface even at moderate air temperature. A retarder holds the mix workable; it does nothing about surface evaporation, which is a curing problem.
The two most common retarder mistakes on prairie pours:
- Over-dosing on a cool day. A dose calibrated for 28 °C, used on a 14 °C morning, can push final set past the point where the finishing crew can get back on the slab in a normal shift.
- Treating a retarder as a haul-time fix. Long hauls and hot loads are better solved by mixing on site than by chemically stalling a truck. On-site volumetric batching removes the drive time from the equation entirely, which is why we batch at the site rather than at a plant across town.
Air entrainment is a separate system
Air-entraining admixtures are specified under ASTM C260, not C494, and they are not optional on exterior Alberta flatwork. Concrete Saskatchewan’s guidance puts recommended air content at 5–8% for nominal maximum aggregate size of 14 mm to 20 mm, which matches what freeze-thaw exposure classes require.
Two things to hold onto:
- Air costs strength. Roughly 5% strength reduction for each 1% of air added, in high-cement mixes. That loss is already accounted for in a properly designed mix; it becomes a problem when air is added late in the field without adjusting anything else.
- Admixtures interact. High-range water reducers, some accelerators and certain supplementary cementing materials all change how an air-entraining admixture performs. This is the single most common reason a load arrives at the right slump and the wrong air content.
That interaction is exactly why admixtures are dosed as a package by the supplier rather than picked one at a time from a shelf.
What changes when the concrete is hot mix concrete
Hot mix concrete — where mix water and sometimes aggregate are heated to raise the delivered temperature — changes admixture behaviour before the truck reaches the site. Higher concrete temperature accelerates hydration on its own, which shortens the finishing window and amplifies the effect of any accelerator in the mix.
The practical consequences on a winter Calgary pour:
- An accelerator dose sized for ambient-temperature concrete may be unnecessary, or actively unhelpful, in hot mix concrete.
- Retarders and slump-retaining Type S admixtures become more useful, not less, because the heat is eating the working window.
- Air content needs checking at the point of placement, not only at the plant, because elevated temperature affects the air-void system.
Batching on site rather than at a distant plant makes this manageable: the delivered temperature is set at the moment of mixing rather than being whatever survived the drive.
FAQ
What is the difference between a plasticizer and a superplasticizer? Terminology, mostly. A plasticizer is a normal-range water reducer — ASTM C494 Type A, 5% minimum water reduction. A superplasticizer is a high-range water reducer, Type F or G, which must reduce water by at least 12%. The performance gap between them is large enough that they are not interchangeable in a mix design.
Can admixtures be added at the job site? High-range water reducers frequently are, because their slump increase is short-lived and site addition puts the peak workability where it is needed. Any site addition has to be at a known dose, mixed for the specified number of revolutions, and recorded on the batch ticket. Adding water at the site instead is a different matter entirely — that changes the water-to-cementing-materials ratio and the strength that goes with it.
Do admixtures let you skip curing? No. Admixtures change the rate of hydration and the water demand; curing supplies the moisture and temperature hydration needs. The CSA A23.1 curing regimes apply to admixtured concrete exactly as they apply to plain concrete.
Is calcium chloride still allowed in Alberta concrete? In plain, non-reinforced concrete, within limits — commonly capped at 2% by weight of cement. It should not be used in prestressed concrete or where aluminum or galvanized metal is embedded, and many owner specifications prohibit chloride-based accelerators outright. Non-chloride accelerators are the default for anything reinforced.
Getting the admixture package right for your pour
The mix design and the admixture package should be decided together, with the placement conditions on the table: temperature, haul distance, finishing crew size, reinforcement congestion, and what the slab has to resist in year twenty. Tell us the conditions and we will build the mix around them, then batch it on site so the concrete arrives at the temperature and slump it was designed for.
Sources
- ASTM International, ASTM C494/C494M-19 Standard Specification for Chemical Admixtures for Concrete — https://www.astm.org/Standards/C494.htm
- Concrete Saskatchewan, Tech Tip #15 — Chemical Admixtures for Concrete — https://concretesask.org/images/techtips/Tech%20Tip%2015%20-%20Chemical%20Admixtures%20for%20Concrete.pdf
- Manitoba Infrastructure, Specification 1030 — Reinforced Cast-in-Place Concrete — https://www.gov.mb.ca/mti/contracts/pdf/manual/1030.pdf